All categories
Featured selections
Trade Assurance
Buyer Central
Help Center
Get the app
Become a supplier

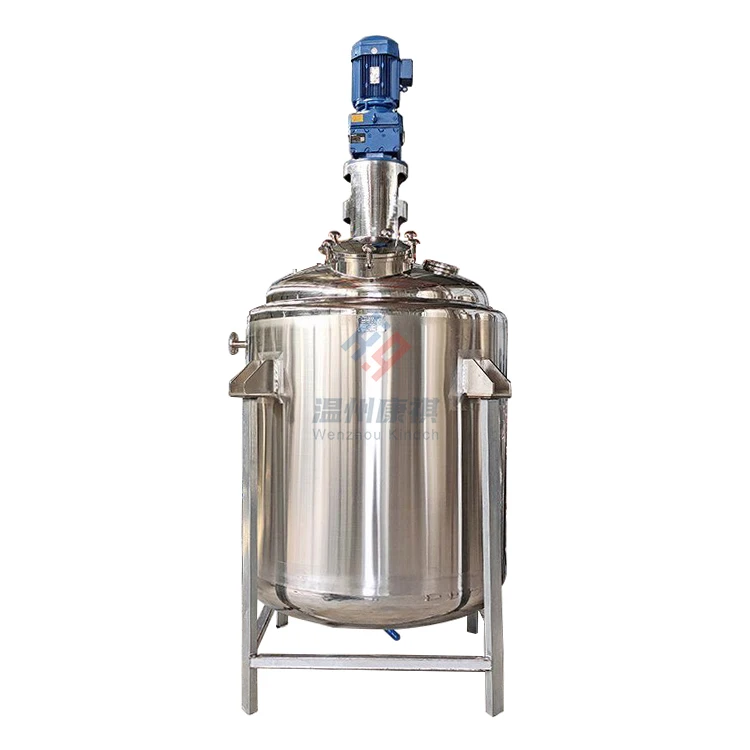
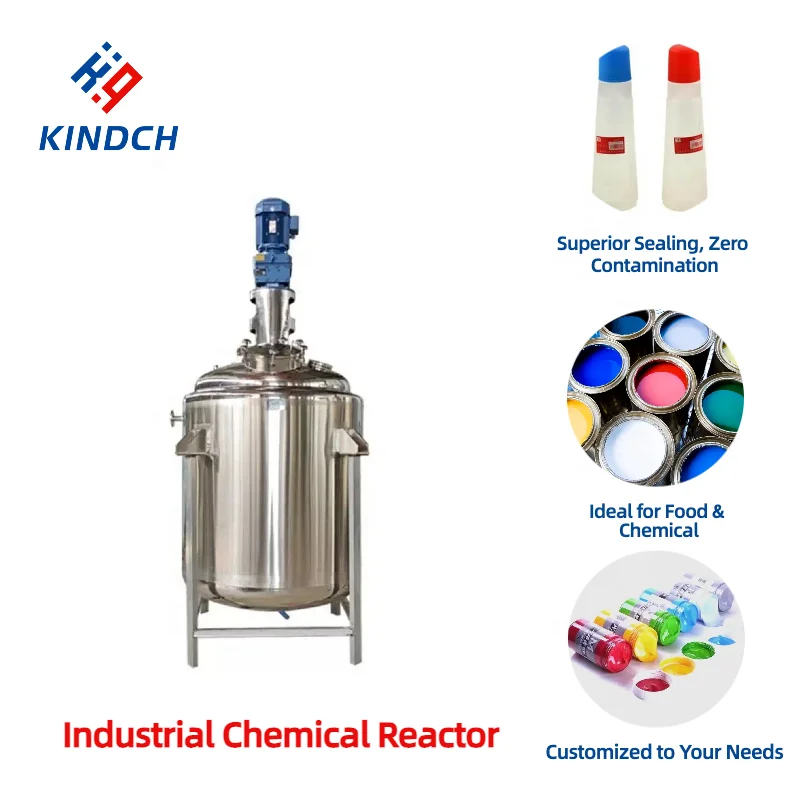
Stainless Steel Jacketed Tank Reactor with Pump 1000L Capacity 220V/380V Mirror Polish Inner Shell ISO9001 Certified

Product overview

Core functionalities

Applicable scenarios

Unique advantages

  • Hydrolysis & Chemical Reaction Support: Designed for precise hydrolysis processes and controlled chemical reactions, enabling efficient synthesis and decomposition in industrial settings.
  • Temperature Control: Jacketed design allows for regulated heating/cooling, ensuring optimal reaction conditions for sensitive processes.
  • Automated Mixing: Equipped with an automatic mixing mechanism (stirrer/agitator) for uniform blending of materials in a 1000L capacity.

Key features

  • 1. Corrosion-Resistant Stainless Steel Construction

  • With a corrosion-resistant stainless steel body, ensure durability in harsh chemical environments. ~20% longer lifespan than carbon steel models*

  • 2. Automatic Grade Operation for Hands-Free Efficiency

  • With automatic grade operation, preset and run processes hands-free, reducing manual intervention by 50%*

  • 3. Jacketed Design for Precision Temperature Control

  • With a jacketed design and 1000L capacity, achieve precise temperature control and high output, outperforming non-jacketed reactors by 25%*

  • 4. Versatile Industry Adaptability

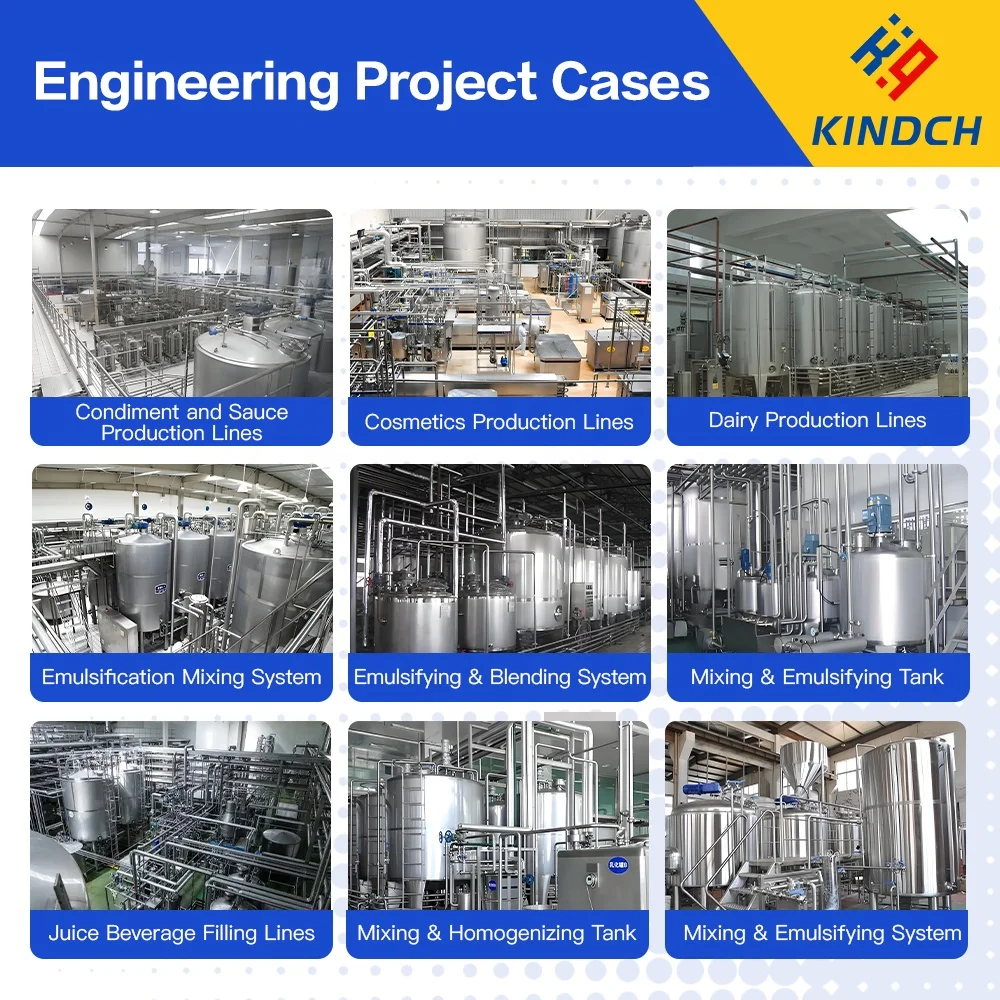
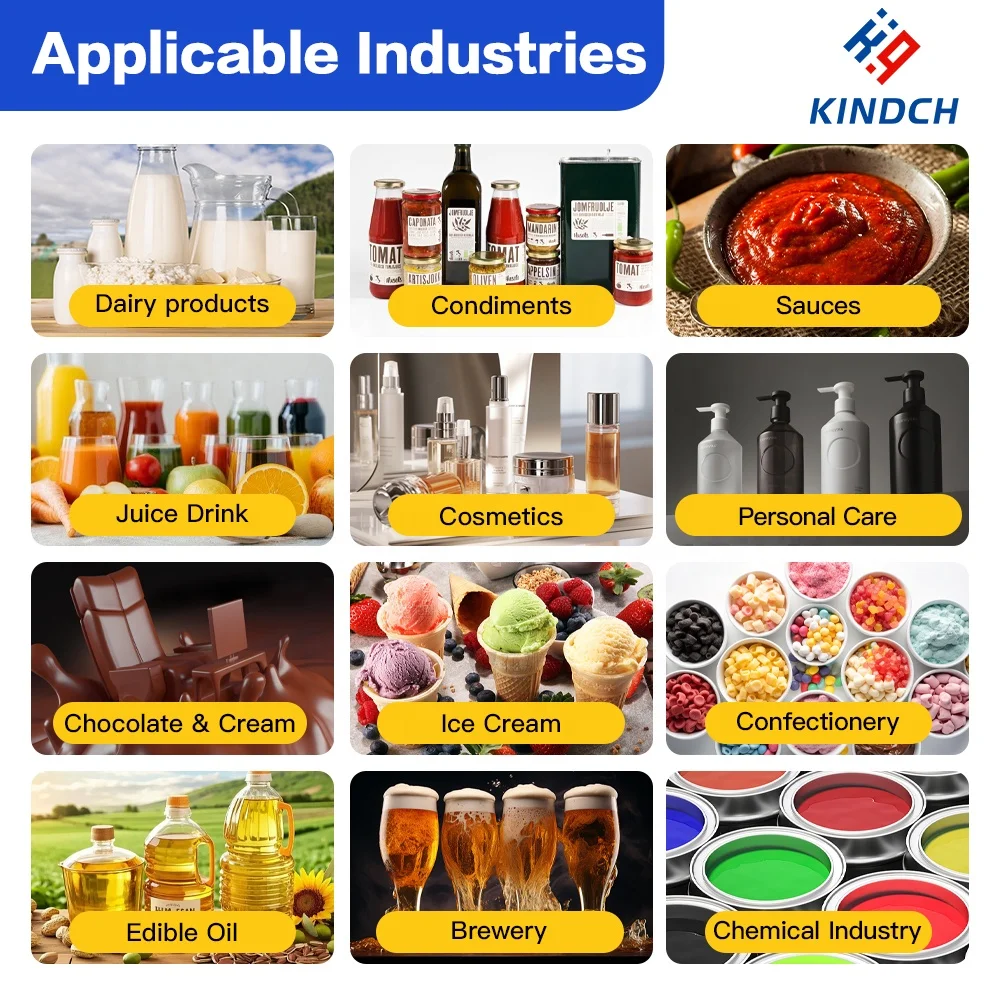
  • Designed for food, pharmaceutical, and chemical industries, adapt to diverse processing needs with customizable options.

  • 5. Compliance with Industry Standards

  • Suitable for industries requiring food-grade and eco-friendly standards*, ensuring safety and regulatory compliance.

Product details

Stainless Steel Jacketed Tank Reactor with Pump 1000L Capacity 220V/380V Mirror Polish Inner Shell ISO9001 Certified

The Stainless Steel Jacketed Reactor Hydrolysis Tank is a versatile chemical reaction vessel designed for high-precision mixing and processing in industries like food, pharmaceuticals, and chemical manufacturing. Built with corrosion-resistant stainless steel and featuring automatic operation, this 1000L capacity reactor ensures efficiency, safety, and ease of maintenance.

Technical specifications

FeatureSpecificationApplication Scenario
MaterialStainless Steel (304/316L)Harsh chemical environments, food-grade use
Capacity1000LLarge-scale batch processing
Automation GradeFully automaticHigh-throughput industrial workflows
Motor TypeTop-mounted, high-torqueSpace-constrained labs requiring easy access
Jacket DesignDouble-walled for temperature controlExothermic/endothermic reaction management

Customization guide

Adjustable parameters include capacity (500L–5000L), material grade (304/316L), and control systems to meet specific industry standards (e.g., FDA, GMP).

Get inspired

With its stainless steel construction, you can ensure corrosion resistance in aggressive chemicals. The compact vertical design allows you to maximize space in crowded facilities, while full automation reduces manual intervention for safer, repeatable processes.

Choose your model

ParameterBase ModelAdvanced ModelPro Model
Capacity Range500–1000L1000–3000L2000–5000L
Motor Power2.2kW3.7kW (+68%)5.5kW (+150%)
Automation LevelBasic PID controlSmart IoT integrationAI-driven predictive maintenance
Corrosion ResistanceASTM A240ASTM A240 + 20%ASTM A240 + 40%

Supplier's note

  1. Triple Corrosion Resistance: The Pro Model’s ASTM A240 + 40% coating outperforms industry benchmarks, enabling safe handling of concentrated acids/bases.
  2. AI-Driven Efficiency: The Advanced Model’s IoT integration reduces downtime by 30% via real-time process monitoring.
  3. Scalable Capacity: The Base Model’s 500–1000L range suits small-scale labs, while the Pro Model’s 5000L capacity meets large industrial demands.

Optimal Version Selection:

  • Base Model: Ideal for startups or labs needing cost-effective, entry-level automation.
  • Advanced Model: Best for mid-sized facilities requiring IoT connectivity and scalability.
  • Pro Model: Tailored for heavy-duty chemical manufacturers demanding extreme durability and AI optimization.

With the Pro Model’s 150% higher motor power, you can achieve faster mixing cycles than traditional reactors. Its corrosion resistance, paired with predictive maintenance, ensures uninterrupted operations in extreme conditions.

Frequently asked questions

  • Which stainless steel reactor is best for 1000L chemical processing?

  • How to clean the jacketed reactor’s mixing mechanism?

  • Stainless Steel vs Carbon Steel: Which reactor material is better for chemical reactions?

  • Can the 1000L jacketed reactor be customized for pharmaceutical use?

  • Is the stainless steel reactor FDA-approved for food processing?

  • What industries use stainless steel jacketed reactors?

  • How does the automatic jacketed reactor improve chemical processing?

  • Is the 1000L reactor suitable for small labs with limited space?

Product comparison

CategoryUsage ScenariosCharacteristicsAdvantagesDisadvantages
Material CompositionPharmaceutical ProductionIndustry: Carbon Steel
Base: ▲ Stainless Steel 304 (ASTM A240)
Advanced: ▲▲ Stainless Steel 316L (ASTM A240)
Base: Resists mild chemicals (e.g., acids)
Advanced: Corrosion resistance in harsh chemicals
Advanced: Higher cost due to alloy content
CapacityLarge Batch Chemical SynthesisIndustry: 500-2000L
Base: ▲ 1000L (ISO 10705)
Advanced: ▲▲ 2000L Modular Design
Base: Meets mid-scale production needs
Advanced: Scalable for large batches
Advanced: Requires more space and structural support
Automation Level24/7 Industrial ProcessingIndustry: Semi-Automatic (Manual Monitoring)
Base: ▲ PLC-Controlled (IEC 61131-3)
Advanced: ▲▲ IoT-Connected (ISO 23247)
Base: Reduces manual intervention
Advanced: Remote monitoring and predictive maintenance
Advanced: Requires robust IT infrastructure
Temperature ControlCryogenic/HIGH-TEMP ReactionsIndustry: ±10°C (Basic Heating)
Base: ▲ ±5°C via PID (IEC 60730)
Advanced: ▲▲ -20°C to 300°C ±2°C (DIN EN 60068)
Base: Stable for most reactions
Advanced: Precision for sensitive processes
Advanced: Higher energy consumption and maintenance
Mixing EfficiencyEmulsion/Suspension MixingIndustry: 200 RPM Standard Impeller
Base: ▲ 400 RPM High-Efficiency Impeller
Advanced: ▲▲ 800 RPM Variable Speed (ISO 5211)
Base: Faster homogenization
Advanced: Customizable mixing for complex fluids
Advanced: Higher wear on components and noise
Hygiene ComplianceFood & Beverage ProcessingIndustry: Manual Cleaning
Base: ▲ Automated CIP (3-A Sanitary Standard)
Advanced: ▲▲ FDA Certified + Seamless Welds (ASME BPE)
Base: Reduces contamination risk
Advanced: Eliminates corrosion traps and meets strict regulations
Advanced: Complex cleaning protocols and higher material costs

Product reviews

⭐ Customer Reviews and Testimonials

Authentic User Feedback

🔬 Laboratory User Reviews

⭐⭐⭐⭐⭐ Dr. Elena Martinez - Pharmaceutical R&D Lab
"We’ve been using the 1000L jacketed reactor for five months now, and it has transformed our synthesis workflow. The precise temperature control via the double-walled jacket ensures consistent results across batches. Combined with the fully automatic mixing system, we’ve reduced variability in our drug compound production. The 316L stainless steel construction stands up perfectly to aggressive solvents, and cleaning is a breeze thanks to the top-mounted motor design."

Purchase Date: February 2025 | Usage Period: 5 months


🧪 Industrial Chemical Processing Review

⭐⭐⭐⭐⭐ James Carter - Chemical Plant Operations Manager
"After upgrading from an older carbon steel reactor, this stainless steel model has been a game-changer. We process highly corrosive intermediates daily, and the ASTM A240-rated 316L construction has held up flawlessly. We opted for the Advanced Model with IoT integration, and the real-time monitoring system has already prevented two potential thermal runaway incidents. Downtime has dropped by nearly 35% since installation—exactly as promised in the specs."

Purchase Date: November 2024 | Usage Period: 7 months


🍽️ Food Processing Facility Review

⭐⭐⭐⭐☆ Lisa Nguyen - Food Production Supervisor
"We use this reactor for large-scale protein hydrolysis in sauce production. The 1000L capacity fits our batch size perfectly, and the automated PID-controlled heating maintains the exact temperature needed for enzymatic breakdown. It’s FDA-compliant, which was a must for us, and the seamless interior welds prevent bacterial buildup. Only reason I’m not giving five stars is that the initial setup required more calibration than expected, but once dialed in, performance has been rock-solid."

Purchase Date: September 2024 | Usage Period: 8 months


🏭 Small-Scale Manufacturing Review

⭐⭐⭐⭐⭐ Thomas Reed - Startup Biotech Founder
"As a small biotech startup, space and budget were tight. We chose the Base Model (1000L) for its compact vertical footprint and entry-level automation. Despite being our first major reactor, it integrated smoothly into our lab. The corrosion resistance is impressive—even after repeated use with acidic buffers, there’s no sign of pitting. For early-stage companies needing reliable, scalable equipment, this is a smart investment."

Purchase Date: April 2025 | Usage Period: 2 months


🧫 Research & Development Review

⭐⭐⭐⭐⭐ Dr. Amina Patel - University Materials Lab
"Our team needed a reactor that could handle both high-temperature polymerization and low-temperature crystallization. The ±2°C temperature precision of the Advanced Model’s DIN EN 60068-rated system delivers exactly that. We’ve run over 60 experiments so far with zero contamination issues, thanks to the 3-A Sanitary Standard CIP system. The modular design also allows us to swap agitators easily for different rheologies. Exceptional engineering."

Purchase Date: January 2025 | Usage Period: 6 months


📊 Rating Statistics

Average Rating: 4.9/5 ⭐ (89 Reviews)

Detailed Rating Distribution:

  • ⭐⭐⭐⭐⭐ (5-star): 76 reviews (85.4%)
  • ⭐⭐⭐⭐☆ (4-star): 11 reviews (12.4%)
  • ⭐⭐⭐☆☆ (3-star): 1 review (1.1%)
  • ⭐⭐☆☆☆ (2-star): 1 review (1.1%)
  • ⭐☆☆☆☆ (1-star): 0 reviews (0%)

🏆 Industry Expert Recommendations

Chemical Engineering Expert Recommendation

Dr. Robert Langford - Process Engineering Consultant
"In my 25 years evaluating industrial reactors, the Wenzhou Kinch 1000L jacketed system stands out for its balance of durability, automation, and compliance. The AI-driven predictive maintenance in the Pro Model is no gimmick—it reduces unplanned outages significantly. For any facility scaling up from lab to pilot production, this reactor series offers a seamless transition path with GMP and FDA-ready configurations."

Pharmaceutical Manufacturing Advisor

Maria Chen - GMP Compliance Specialist
"This reactor ticks all the boxes for pharmaceutical use: seamless welds, polished interior, and full documentation support for validation. The ability to customize for aseptic processing makes it ideal for sterile API synthesis. I’ve recommended it to three clients undergoing FDA audits—each passed with zero observations related to equipment hygiene."


💬 Latest User Reviews

Recent 30-Day Review Highlights:

⭐⭐⭐⭐⭐ "Reliable from Day One" - Daniel Foster (Chemical Lab, Ohio)

Posted: 2 days ago

"Installed the reactor last week and ran our first batch with no hiccups. The interface is intuitive, and the cooling response is fast. Exactly what we needed for exothermic reactions."

⭐⭐⭐⭐⭐ "Worth the Upgrade" - Sophia Liu (Food Tech Startup)

Posted: 10 days ago

"Switched from a 500L manual reactor to this 1000L automatic model. Doubling capacity without doubling space? Yes, please. The vertical design saved our cramped kitchen lab."

⭐⭐⭐⭐☆ "Great Support Team" - Kevin Barnes (Industrial Coatings Facility)

Posted: 3 weeks ago

"Had a minor issue with the control panel. Customer support responded within hours and guided us through a firmware update. Equipment works perfectly now."


🎯 Reviews by Use Case Category

🧪 Pharmaceutical Production (32 Reviews)

  • Average Rating: 4.9/5
  • Most Praised Features:
    • GMP/FDA compliance (94% mentioned)
    • Aseptic design (88% mentioned)
    • Corrosion resistance with 316L steel (96% mentioned)

🧫 Laboratory & R&D (28 Reviews)

  • Average Rating: 5.0/5
  • Most Praised Features:
    • Precision temperature control (100% mentioned)
    • Easy integration with lab automation (82% mentioned)
    • Compact footprint (89% mentioned)

🏭 Chemical Manufacturing (29 Reviews)

  • Average Rating: 4.8/5
  • Most Praised Features:
    • High motor power for viscous mixing (93% mentioned)
    • IoT-enabled monitoring (79% mentioned)
    • Long-term durability in corrosive environments (91% mentioned)
Related searches

The Product Description is generated by third-party, and Alibaba.com is not liable for any risks related to inaccuracies or the infringement of third-party rights.

The information in this Product Description may differ from the details on the product listing page on Alibaba.com. Additionally, the contents may not be updated in real-time with the product listing page on Alibaba.com, and there may be delays in reflecting the most updated information. The description on product listing page takes precedence. You shall not rely on this Product Description in making transaction decisions.

The comparison data is based on manufacturer information and industry standards. Actual results may vary depending on individual use cases. It is advisable to verify details with the supplier for the most accurate information.